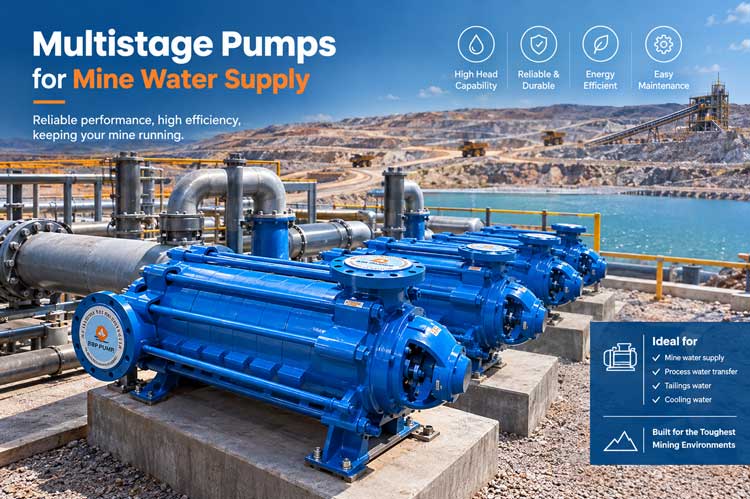
Mining operations depend on a reliable, uninterrupted water supply for everything from dust suppression and ore processing to personnel facilities and equipment cooling. When a mine sits hundreds of meters below the surface — or when water must be pushed across miles of rugged terrain — standard single-stage centrifugal pumps simply cannot deliver the pressure head required. That is where multistage pumps become indispensable.
This complete selection guide walks mining engineers, procurement teams, and facility managers through every critical decision: understanding how multistage pumps work, identifying the right pump type, calculating performance requirements, choosing materials for aggressive mine water, and avoiding the costly mistakes that lead to premature failure.
A multistage pump is a centrifugal pump containing two or more impellers (stages) arranged in series within a single casing. Each stage adds pressure (head) to the fluid before passing it to the next. The result is a pump capable of generating very high discharge pressures from a compact, energy-efficient package.
Related reading: What is a Multistage Centrifugal Pump?
Mine water supply challenges are unique:
A correctly selected multistage pump addresses all four challenges simultaneously, delivering the total dynamic head (TDH) needed while remaining compact enough to install in confined underground pump stations.
The most common configuration for surface water supply stations, these pumps feature impellers mounted on a single shaft inside a barrel or ring-section casing. They are easy to maintain, accept standard motor configurations, and allow impeller staging to be adjusted by adding or removing sections.
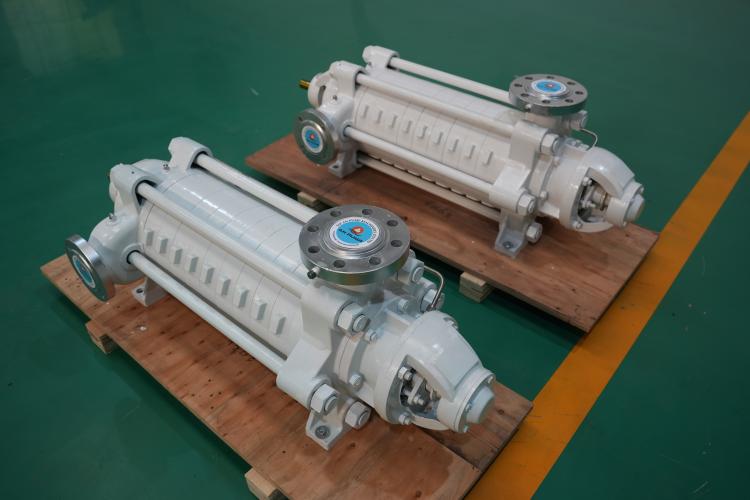
Best for: Surface booster stations, process water supply, long-distance pipeline boosting.
Vertical turbine pumps suspend a column of staged impellers directly in a borehole or sump. The motor sits at the surface while the pump stages operate submerged. This eliminates suction-lift limitations and makes them ideal for dewatering sumps that double as supply reservoirs.
Best for: Underground pump stations, dewatering sumps repurposed for supply, deep boreholes.
Entirely submerged units with a close-coupled motor sealed for underwater operation. Installation is fast, there is no need for a pump house at shaft level, and cavitation risk from suction lift is eliminated.
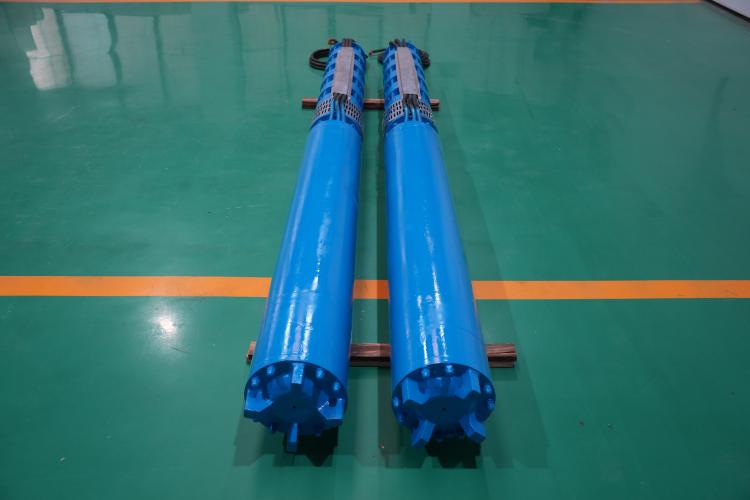
Best for: Emergency supply pumping, remote underground water points, temporary mine development supply.
A ruggedized variant of the horizontal multistage design, enclosed in a welded barrel casing that contains extreme pressures. These are used where system pressures exceed 120 bar — common in very deep mines with water columns exceeding 1,000 meters.
Best for: Ultra-deep shafts, high-pressure fire suppression supply, deep cooling water circuits.
Choosing the wrong pump for a mine water supply application results in energy waste, shortened service life, unplanned downtime, and safety risks. Follow these steps in sequence.
TDH is the total pressure the pump must overcome, expressed in meters of water column (mWC) or bar:
TDH = Static Head + Friction Losses + Minor Losses + Residual Pressure Requirement
Rule of thumb: Add a 10–15% safety margin to your calculated TDH before selecting a pump model. Mine piping systems evolve, and a pump with headroom handles future extensions without replacement.
Calculate peak demand, not just average demand. Mine water supply must meet simultaneous worst-case consumption:
Apply a demand diversity factor based on shift patterns and operational schedules to avoid oversize — oversized pumps operating at reduced flow risk recirculation damage and accelerated wear.
Overlay the system curve (TDH versus flow rate for your piping network) with the pump performance curve (head versus flow rate from the manufacturer). The intersection point — the operating point — must fall within the pump's preferred operating region (typically 70–110% of the best efficiency point, or BEP).
Operating consistently far left of BEP causes recirculation and cavitation; operating far right overloads the impellers and motor. Both conditions sharply reduce service intervals.
Cavitation is among the most destructive forces acting on pump internals. Calculate NPSHa for your installation:
NPSHa = (Absolute pressure at suction source) − (Vapor pressure of water at operating temperature) − (Friction loss in suction piping) − (Static suction lift)
The pump's required NPSH (NPSHr) from the manufacturer's data sheet must be at least 0.5–1.0 m lower than your NPSHa. In high-altitude mines, where atmospheric pressure is reduced, this calculation becomes critical and often dictates selection of a submersible or vertical turbine pump over a surface horizontal unit.
Mine water chemistry varies dramatically by geology and mining method. Conduct a full water analysis before specifying materials:
| Contaminant | Risk | Recommended Material |
|---|---|---|
| Sulfates > 250 mg/L | Sulfate attack on seals and coatings | 316L stainless steel casings, EPDM seals |
| Chlorides > 200 mg/L | Pitting and crevice corrosion | Duplex stainless steel (2205) or super duplex |
| pH < 6.0 (acid mine drainage) | Accelerated corrosion of iron components | Duplex stainless, HDPE-lined casings |
| Suspended solids > 50 mg/L | Abrasive impeller wear | Hardened chrome iron impellers, wear rings |
| Total hardness > 500 mg/L | Scaling inside casing | Electropolished internals, scale inhibitor dosing |
Never assume mine water is clean. Even clear-appearing underground water can carry dissolved ionic loads that destroy standard cast iron or bronze pump internals within months.
Mine water supply pumping is often the single largest energy consumer in an underground operation. Optimizing pump selection for efficiency delivers measurable cost savings over the mine's life.
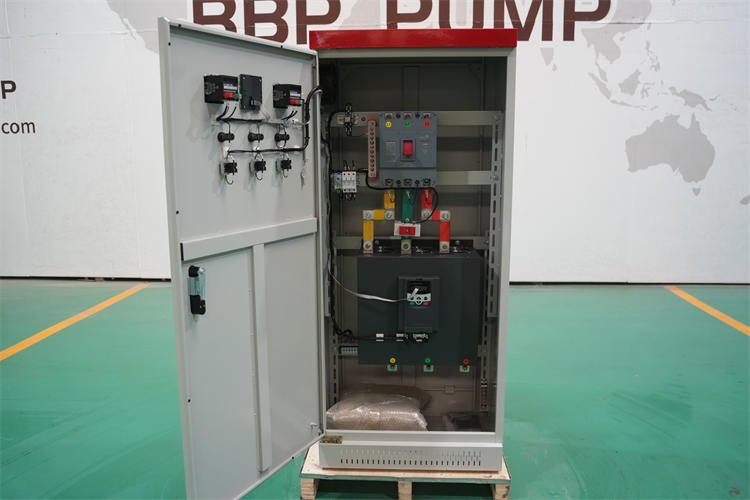
Fitting a multistage pump with a VSD allows rotational speed — and therefore head and flow — to follow actual demand. The affinity laws show that reducing pump speed by just 20% cuts power consumption by nearly 50%. For mines with highly variable demand profiles, VSDs typically deliver payback periods of 12–24 months.
Rather than one oversized pump, consider two or three smaller multistage units in parallel. This allows the operation to run one pump during low demand and bring additional units online as demand rises. Parallel configurations also provide built-in redundancy — a critical safety requirement in underground mining environments.
Most ring-section horizontal multistage pumps allow impeller stages to be removed without replacing the entire unit. If the mine expands and pipeline friction increases, stages can be added. This "right-sizing" approach prevents the chronic inefficiency of a pump running far from its BEP.
Even a perfectly selected pump will fail prematurely if installed incorrectly.
Foundation and alignment: Horizontal multistage pumps require a rigid, level concrete foundation. Shaft misalignment between pump and motor exceeding 0.05 mm causes bearing failure within weeks in continuous-duty mine applications.
Suction piping: Suction piping must be at least one nominal diameter larger than the pump inlet and should rise continuously toward the pump to prevent air pockets. Gate valves, not globe valves, should isolate the suction line.
Pressure relief and bypass: Always install a pressure relief valve downstream of the pump, set to 110% of the maximum system operating pressure. A bypass line allows the pump to run against a closed discharge during commissioning and flushing without water hammer damage.
Commissioning flush: Flush the entire pipeline system with clean water — discarding the first volume — before passing through the pump. Construction debris and weld slag destroy mechanical seals and wear rings instantly.
Multistage pumps in mine water supply service typically run 6,000–8,760 hours per year. Planned maintenance intervals must reflect this duty.
Maintaining a spare rotating element (shaft, impellers, and wear rings assembled as a cartridge) dramatically reduces unplanned downtime. In continuous mining operations, a pump pulled for inspection can be back in service within hours if a spare element is ready for installation.
Mine water supply systems are subject to national and local mining safety regulations. In most jurisdictions, the following requirements apply:
Consult the applicable mining regulations for your jurisdiction and ensure the selected pump package is fully documented for regulatory review.
Underestimating future head requirements. Mines deepen and pipelines extend. Select a pump with spare stages available, or a casing rated for head values 20–30% above current requirements.
Ignoring water temperature. Hot water in deep mines — particularly in geothermally active regions — reduces NPSHa, lowers water density, and degrades seal materials. Account for water temperature in all hydraulic calculations.
Specifying insufficient motor service factor. Mine water supply pumps routinely start under load, experience voltage fluctuations, and run in high-ambient-temperature environments. Specify motors with a service factor of at least 1.15 and insulation class F minimum.
Over-relying on a single vendor's selection software. Pump selection tools are valuable starting points, but a mine water system has unique characteristics that require engineering judgment. Always validate software outputs against manual hydraulic calculations.
Selecting a multistage pump for mine water supply is an engineering exercise that spans hydraulics, materials science, electrical systems, and regulatory compliance. The stakes are high — an undersized or incorrectly specified pump doesn't just inconvenience operations; it can halt production, compromise worker safety, or create environmental liabilities.
Follow the structured selection methodology in this guide: define TDH accurately, match flow to real demand, verify NPSH margins, specify materials for actual water chemistry, and plan for energy efficiency from day one. Pair the correct pump with proper installation practices, a documented maintenance schedule, and regulatory compliance, and your mine water supply system will deliver decades of reliable service.
For complex installations — particularly those involving ultra-deep mines, highly corrosive acid mine drainage, or combined supply and dewatering functions — engage a specialist pump engineer early in the design process. The cost of expert engineering input is a fraction of the cost of a misapplied pump in a critical underground environment.
